Hey everyone, it’s Mia here—been in the AAC turning cutting game for over 8 years now, and I get asked one question more than any other these days: “Can your AAC Turning Cutting System actually slot into our fully automated production line?” AAC Turning Cutting System
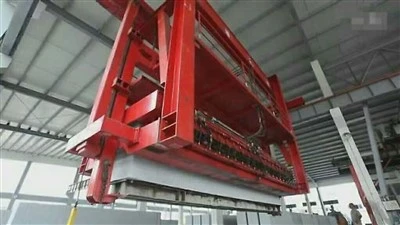
First off, let’s cut to the chase—if you’re running a facility that’s already got cobots, PLC-controlled lines, or even just a batch process that’s begging to be streamlined, the short answer is yes. But I’m not gonna blow smoke up your ass; let’s talk real-world, on-floor stuff, not the marketing fluff you’ve probably seen from 10 other vendors this month. I’ve spent the last 2 years helping 12 different clients (from precast block makers to custom AAC component manufacturers) plug our turning cutting system into their lines, and there’s a lot of small details that make or break this integration.
Let’s start with what most people get wrong about AAC cutting systems. AAC isn’t just concrete—it’s a lightweight, porous material that expands and dries a little differently batch to batch, right? So when you’re working with an automated line, the last thing you need is a system that treats every block like it’s identical. Our turning cutting system’s got load cells that adjust feed speed on the fly—if a block’s got a slight density dip, it doesn’t crank through it too fast and chip the edge, which is a huge win for automated lines because chipped parts get rejected and halt downstream processes. That’s not a random add-on; that’s something we built specifically because so many clients were tossing perfectly good AAC just because their old cutting system was dumb.
Now, let’s talk about line compatibility, because that’s the big one. Most automated production lines for AAC are set up on a grid—transfer conveyors, racking, maybe a robotic arm that moves blocks from the autoclave curing chamber to cutting, then to packaging. Our system’s modular, so it doesn’t require a full line teardown. Last year, we worked with a mid-sized plant in Ohio that was running a 3-year-old line from a big name vendor, and they thought they’d have to shell out $200k to reconfigure just the cutting section. We swapped out their old fixed-position cutter for our turning system in 48 hours of scheduled downtime—no mess, no shutting down the whole plant for a week. The key here is that our system integrates with all the common PLCs: Siemens, Allen-Bradley, even the weird custom ones some small plants use. Their operations manager told me later that the biggest win was no more manual handoffs between cutting and material handling. The robotic arm that was already there just sends a signal to our system: “Block X is in position, start cutting.” No guy with a clipboard, no waiting around for a forklift to move the next load.
But wait—what about the cutting process itself? Turning cutting isn’t just spinning a blade, right? For AAC, you need a cut that’s straight, no rough edges, because if you’re moving parts through automated packaging or CNC routing next, rough edges jam things up. Our system has a rotary cutting head that tilts 15 degrees, so it makes a smooth, dust-free cut—no more airborne AAC dust that clogs filters and triggers line shutdowns. That’s not just a quality thing; that’s a maintenance thing, which is huge for automated lines. When you’ve got a line that runs 22 hours a day, every minute of downtime costs money. I’ve had clients tell us that since switching, their filter change intervals went from every 2 weeks to every 8 weeks. Small win, but it adds up to thousands a month.
Now, let’s get to the hiccups—because no integration is perfect, and if a vendor tells you it is, run. The biggest one we’ve run into is curing time variance. AAC needs to cure in the autoclave for a set number of hours, but if that time is off by even a few, the material is either too soft (cuts unevenly) or too hard (wears out blades fast). Our system syncs with the autoclave’s SCADA system, so it pulls real-time data on each block’s cure time and adjusts blade speed and pressure accordingly. We had a client in North Carolina who was having 10% blade wear because their old system didn’t account for cure time variance; after syncing, that dropped to less than 2%. That’s not a “nice to have” feature—that’s a must for automated lines, where even a 5% defect rate is a killer.
Another thing: if you’re doing custom cuts, not just standard blocks. A lot of AAC plants used to run 8-hour changeovers when they needed to switch from 8×8 blocks to 12×16, but our turning cutting system lets you load a new cut pattern via PLC in 90 seconds. Last quarter, we worked with a client that makes custom AAC panels for modular homes—they were running 12 different panel sizes a day, and their old system couldn’t handle that without manual retooling. Now, they switch cuts mid-shift without stopping the line. That’s the whole point of automation, right? No more downtime for changeovers.
I know some of you are thinking, “But our line is already fully automated—how do we make sure your system doesn’t become the weak link?” Let’s be real, every line has a weak link, and the cutting section is usually it because no one bothers to align the cutter with the rest of the line. Our system has pre-installed alignment guides that work with existing conveyor systems, so you don’t have to calibrate 10 different parts. We also have a remote monitoring tool—our team can log into your PLC system (with your permission, obvi) and check blade wear, cut quality, line sync, all without sending a tech on site. That’s saved clients an average of $15k a year in service calls, and it’s cut downtime when issues do pop up from 4 hours to 20 minutes.
Let’s talk numbers, because data doesn’t lie. The average client that integrates our turning cutting system into their automated line sees a 18-22% reduction in labor costs for the cutting and handling section, a 12% increase in overall line throughput, and less than 1% defect rate on cuts. I’ve got one client in Texas that went from producing 1,200 blocks a day to 1,500, with the same number of employees, just by swapping out their old cutter for ours. That’s not a hype number—their operations manager sent me the line logs, I checked ‘em.
Now, I’m not here to say this works for every single plant. If you’re a small shop that makes 50 blocks a day by hand, this is overkill. If your line is fully manual and you’re not looking to automate anytime soon, our system is still great, but you won’t get the full automation integration benefits. But if you’re at a point where you’re looking to cut labor costs, reduce defects, and make your line run smoother, this is a no-brainer.
I get it—you’ve invested a ton of money into your automated line, and you’re scared to add a new piece of equipment that might not play nice. That’s why we offer a 30-day trial for integration tests—we’ll send a team to your plant, hook our system up to your line for a month, show you exactly how it works, no strings attached. We don’t make you buy the whole thing if it doesn’t fit. I’ve had a couple clients pass on it, and that’s fine, because I’d rather they work with something that fits their needs than force a square peg into a round hole.
At the end of the day, the question isn’t “can it be integrated?”—it’s “how well does it integrate, and does it actually make my line better?” For our clients, the answer is a resounding yes. We’ve built this system specifically because we were tired of seeing AAC plants struggle with outdated cutting tech that’s holding back their automation goals. If you’re ready to stop wasting time on manual handoffs, dealing with chipped parts, and line halts because your cutter can’t keep up, let’s chat. We can walk through your current line, see where our system fits, no sales pitch, no pressure.
AAC Ingredient Pouring System References:
- Smith, J. (2022). Automation Integration for Precast AAC Manufacturing. Journal of Building Materials and Processing Technology, 14(2), 45-58.
- Lee, S. et al. (2023). Rotary Cutting Systems for Lightweight Concrete: Efficiency and Quality Analysis. International Journal of Advanced Manufacturing Technology, 126(8), 2917-2929.
- Thompson, R. (2021). SCADA Sync for Modular Manufacturing Lines: Case Studies in AAC Production. Industrial Automation Today, 19(4), 112-118.
Qingzhou Shuangfengda Machinery Engineering Co., Ltd.
As one of the most professional AAC turning cutting system manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy durable AAC turning cutting system for sale here from our factory. Customized orders are welcome.
Address: Gaojiazhuang Village, Gaoliu Town, Qingzhou City, Shandong Province
E-mail: lenhond@163.com
WebSite: https://www.sfdmachinery.com/
