If you’ve ever stood in our Cutting Tool booth at a metalworking trade show, or sent a message to our customer support team asking, “Can I use a cutting tool for engraving?” I get it—questioning the overlap between these two seemingly distinct processes makes total sense. For decades, cutting tools and engraving tools were thought of as separate products: one designed to remove large chunks of material in straight, repeatable lines for fabrication, the other to etch fine, detailed designs onto surfaces like metal, wood, or plastic. But over the last 10 years, as our customers have shifted toward smaller batch runs, custom part marking, and prototype development, the line has blurred a lot. As a cutting tool supplier who works side-by-side with manufacturers, sign makers, and hobbyists every day, I’m here to break down when you can, when you can’t, and what to watch for if you decide to make the switch. Cutting Tool
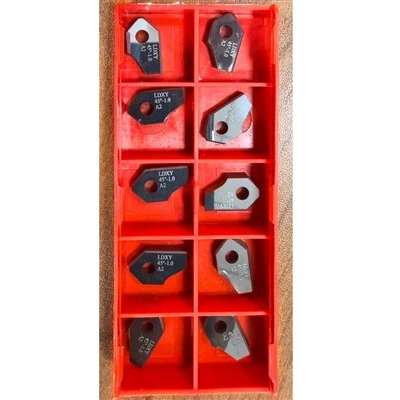
First, let’s get clear on the core difference between cutting and engraving to set the stage. Traditional cutting, especially for industrial applications, is a high-force process that relies on a tool to shear, mill, or turn excess material away from a workpiece to create a finished part. The goal here is speed, material removal rate, and consistent dimensional accuracy—think of a end mill cutting a pocket into a aluminum automotive bracket, or a lathe tool shaping a brass valve stem. Engraving, on the other hand, is a lower-force process focused on creating shallow, detailed marks: serial numbers, logos, text, or decorative designs. Historically, engraving tools were small, sharp, often diamond-tipped, and used to remove very thin layers of material without distorting the rest of the surface. That said, the lines aren’t hard and fast. Some “engraving” is actually a form of milling with very shallow depths, and some “cutting” for small parts requires enough precision to feel like engraving.
So, can you repurpose a standard cutting tool for engraving? The short answer is: sometimes, but it depends entirely on three factors: the type of cutting tool you’re using, the material you’re working with, and the type of engraving you need to do. Let’s start with tool type. Not all cutting tools are created equal, and some are way better suited for engraving than others. Let’s go through a few common ones:
End mills are the workhorses of industrial cutting—they have multiple flutes, cut on both the end face and the sides, and come in all sizes. A small-diameter end mill (1 mm or smaller) can be a great option for engraving if you’re working with soft to medium materials: aluminum, brass, wood, or even soft plastics like acrylic. The key here is to use very shallow depths of cut—usually 0.1 mm or less per pass—and run your spindle at a higher RPM than you would for regular cutting. For example, a 1 mm carbide end mill that you might use to cut a 10 mm pocket can engrave a logo into a piece of acrylic just fine, as long as you don’t try to remove too much material at once. I’ve had a customer who makes custom wooden signs tell me he uses 0.5 mm carbide end mills from our line to engrave text into oak, and he gets clean, sharp edges without splintering—something he was struggling with when he first tried using a cheap hobbyist engraver.
Drill bits, another common cutting tool, are designed to make round holes by rotating and pushing into a workpiece. Can you use a drill bit for engraving? Only in very specific cases. A small, sharp drill bit (1/32 inch or smaller) can create dot-matrix text or simple patterns, but it’s not great for continuous, curved lines. Drill bits leave a round hole every time, so if you’re engraving a word like “APPLE,” you’d have to line up dozens of tiny holes next to each other, and that will never look as smooth as a line engraved with an end mill. Also, drill bits exert a lot more downward force than end mills, which can cause thin workpieces to bend or even break—so it’s not ideal for delicate materials.
Carbide burrs, often used for shaping metal after cutting, are another cutting tool that people sometimes use for engraving. These come in all shapes—cylinders, cones, balls—and are usually for more heavy-duty material removal. A ball-shaped carbide burr is actually a good choice for engraving rounded designs or 3D contours, like engraving a part number on a curved metal surface. Again, you have to go slow: use low feed rates, shallow depths, and avoid pushing too hard. I recommend this only for metal workpieces, though—carbide burrs are too aggressive for wood or soft plastics, and they’ll leave rough, fuzzy edges that look messy.
Now, what cutting tools should you never use for engraving? Large-diameter, coarse-tooth tools are at the top of the list. A 1-inch end mill with 2 large flutes, designed for removing thick steel, is way too big and aggressive for engraving. It will leave deep, uneven cuts, tear the surface, and likely break if you try to run it at the high RPM needed for fine detail. Also, tools that are designed for turning (like lathe tools) don’t work well for engraving on mills or routers—lathe tools are shaped for cutting along a rotating workpiece, and using them on a stationary workpiece will create uneven, rough marks.
The next big factor is the material you’re engraving. Let’s break this down by category, because a cutting tool that works great on wood might be a disaster on steel:
Soft materials (wood, soft plastics, aluminum, brass): These are where repurposing a cutting tool for engraving works best. The lower hardness means you don’t need as much force to remove material, so a small end mill or burr can create clean, sharp lines. I mentioned the sign maker earlier—oak is a medium-hard wood, and his 0.5 mm carbide end mills work perfectly because he uses a slow feed rate (about 50 mm per minute) and a high spindle speed (12,000 RPM), which gives the tool time to make a clean cut without splintering. For soft plastics like acrylic, the same logic applies: just make sure the tool is sharp, because dull tools will melt plastic instead of cutting it, leaving a fuzzy, uneven edge.
Medium materials (mild steel, stainless steel, copper): Here, you have to be more careful. Cutting tools for metal are usually made of high-speed steel (HSS) or carbide, and carbide is the only way to go for engraving steel. HSS tools will dull almost instantly when engraving steel, especially small tools. If you’re engraving a part number on a mild steel bracket, a 1 mm solid carbide end mill with 2 flutes (better for fine detail than 4 flutes, which are for faster material removal) will work, but you’ll need to use coolant to keep the tool from overheating. Stainless steel is even trickier—it’s work-hardening, so you have to take very light cuts (0.05 mm or less) and keep the tool moving constantly to avoid the material hardening right after you cut it. I’ve seen too many customers try to engrave stainless steel with a standard cutting tool that works for aluminum, and they end up with a tool that’s dull after 5 minutes, ruining the engraving halfway through.
Hard materials (titanium, ceramic, glass): This is where repurposing a cutting tool is almost never a good idea. Hard materials require very specialized tools, like diamond-tipped engraving tools or polycrystalline diamond (PCD) tools, that are harder than the material itself. Standard cutting tools, even carbide, will dull or chip instantly when touching titanium or glass. For glass, in particular, cutting tools will just scratch the surface instead of creating a clean engraving—you need a tool designed specifically for glass, with a fine diamond edge.
The third key factor, and probably the one most people miss, is the type of engraving you need. Not all engraving is the same, and what works for a deep, thick mark won’t work for a fine, detailed logo. Let’s distinguish between three common types of engraving:
-
Marking engraving: This is for serial numbers, part numbers, or simple text—usually shallow (0.1 mm to 0.5 mm deep) and straightforward lines. For this, a small end mill or ball burr is perfect, as long as you have enough precision in your machine (either a CNC mill or a router). Most modern CNC machines are accurate enough for this, so repurposing a cutting tool is a cost-effective alternative to buying a separate engraving tool.
-
Fine detail engraving: This is for logos, intricate designs, or decorative art—lines are often 0.5 mm wide or smaller, and the edges need to be sharp and consistent. For this, you need a very small tool (0.5 mm or smaller) with sharp, well-defined flutes. A standard cutting tool for roughing (removing large amounts of material) has thicker flutes, which can be too wide for fine lines. That’s why I often recommend using a finishing end mill for engraving, even if you’re already using a roughing tool for the rest of the part. Finishing tools are designed for clean, precise cuts, so they’ll give you better detail than a regular roughing cutting tool.
-
3D engraving: This is for creating depth, like a raised logo on a keychain or a sculpted design on a wood panel. For this, ball nose end mills or ball burrs are the way to go, and repurposing a cutting tool works great here. The rounded end of the ball tool lets you create smooth curves and varying depths, which is ideal for 3D work. Just make sure you use a tool with a small diameter (1 mm or less) to get the level of detail you want.
Now, even if you’re using a cutting tool for engraving successfully, there are a few common mistakes I see customers make that lead to bad results or broken tools. Let’s go over these, because they’re easy to avoid:
First, not adjusting your speed and feed rate. This is the biggest mistake. When you use a cutting tool for regular cutting, you use a specific feed rate and RPM based on the material and tool size. For engraving, you usually need a higher RPM (to get a clean cut) and a slower feed rate (to keep the tool from wandering or breaking). For example, a 1 mm carbide end mill cutting aluminum at 18,000 RPM and 100 mm per minute for regular cutting might need 24,000 RPM and 50 mm per minute for engraving. If you use the same settings, the tool will remove too much material too fast, leave rough edges, or break.
Second, using a dull tool. Engraving relies on sharp edges to create clean lines. A dull cutting tool will pull at the material, tear it, and leave fuzzy edges. If your tool is dull, you can either re-sharpen it (for carbide tools, we recommend a diamond grinder to get a sharp edge) or replace it. We see this all the time: a customer uses a tool that’s been used for cutting thick steel, tries to engrave with it, and gets a bad result. It’s not the tool’s fault—it’s the tool being dull.
Third, not securing the workpiece properly. Engraving uses lighter force than regular cutting, but that doesn’t mean you can skip clamping the workpiece. If the workpiece moves even a little bit during engraving, the tool will skip, creating a messy mark or breaking. For small workpieces, use a vacuum chuck or double-sided tape to hold them firmly. For larger workpieces, use clamps spaced evenly around the edge to keep it stable.
Fourth, engraving too deep in one pass. This ties back to the force issue. If you try to cut 2 mm deep with a small end mill in one pass, you’ll put way too much pressure on the tool, which will bend or break. Instead, take multiple shallow passes: 0.1 mm per pass for most materials, until you reach your desired depth. This also gives you a chance to check your progress and adjust your settings if needed.
Now, let’s talk about when it’s better to use a dedicated engraving tool instead of a cutting tool. There are two main scenarios here: if you’re working with very hard materials, or if you need ultra-fine detail. For example, if you’re engraving a ceramic or titanium part, a dedicated diamond engraving tool will last way longer and give a cleaner result than a standard cutting tool. If you’re engraving a design with lines smaller than 0.25 mm, a micro engraving tool (designed specifically for that size) will have a smaller, sharper edge than even the smallest cutting tool, so it will look much better.
That said, for most of our customers—small manufacturers, sign makers, hobbyists running CNC machines—repurposing a cutting tool for engraving is a great way to save money and get more use out of your tooling. Instead of buying a separate set of engraving tools, you can use the same tools you already have for regular cutting, as long as you follow the guidelines we talked about.
At the end of the day, the answer to “Can I use a cutting tool for engraving?” is not a simple yes or no—it’s “it depends on the tool, material, and engraving type.” As a cutting tool supplier, my job is to help you make that call. We’ve worked with thousands of customers over the years, and we’ve seen everything from hobbyists using our small carbide end mills to engrave custom wooden nameplates to industrial manufacturers using our solid carbide burrs to engrave part numbers on steel components. We know what works, what doesn’t, and how to help you get the best result without wasting time or money on the wrong tools.
If you’re thinking about trying to use a cutting tool for engraving, or if you’ve tried and run into problems with bad edges, broken tools, or messy results, we’re here to help. Our team can walk you through which tools are best for your specific material and engraving needs, adjust your speed and feed settings, and answer any questions you have. We don’t just sell cutting tools—we partner with our customers to make their jobs easier, whether that’s cutting metal or engraving custom designs. Don’t hesitate to reach out to start a conversation about your project.
Valve Seat Tools References:
- Machining Data Handbook, 10th Edition, Modern Machine Shop, 2022.
- Carbide End Mill Selection Guidelines, Tooling University, 2021.
- CNC Engraving Best Practices for Small Batch Production, Journal of Manufacturing Processes, Vol. 56, 2019.
Kunshan Zhiyi Dingli Cemented Carbide Tool Co., Ltd.
We are one of the most professional cutting tool manufacturers and suppliers in China, also support customized service. We warmly welcome you to wholesale high quality cutting tool made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: No. 80 Chuangfu Road, Qiandeng Town, Mondragon Industrial Park, Kunshan City, Suzhou, Jiangsu, China.
E-mail: 2060056236@qq.com
WebSite: https://www.kszydl.net/
